2026 Best Spunlace Nonwoven Fabric Types for Buyers?
Choosing the right Spunlace Nonwoven Fabric in 2026 requires more than comparing prices. Buyers must examine fiber content, basis weight, tensile strength, absorbency, softness, and production consistency. A fabric that feels smooth on a sample may perform poorly after converting, wetting, or sterilization. No single type wins every application.
This guide introduces practical options, including polyester spunlace, viscose blends, wood-pulp composites, biodegradable fibers, and high-strength industrial grades. Each type offers different benefits. Viscose can provide excellent absorbency, while polyester often supports durability and dimensional stability. Wood-pulp blends may improve liquid handling, but they can require careful process control. Small details matter. Roll width matters. Edge quality matters.
Reliable buying decisions should come from verified technical data, recent samples, and supplier experience. Ask for test reports covering basis weight, microbial control, moisture retention, and strength in both directions. Review certifications that match the intended market and product claim. Factory audits, traceability records, and consistent batch documentation also deserve attention. These steps reduce uncertainty, although they cannot remove it completely.
Cost deserves a wider view. A cheaper roll may create more waste, slower cutting, or customer complaints. Conversely, a premium fabric may exceed the actual performance requirement. This article compares the most useful Spunlace Nonwoven Fabric types for buyers in 2026, while recognizing that recommendations may change with regulations, machinery, and application needs. Some conclusions remain debatable. That is why practical testing should guide the final purchase.
What Is Spunlace Nonwoven Fabric and How Is It Made?
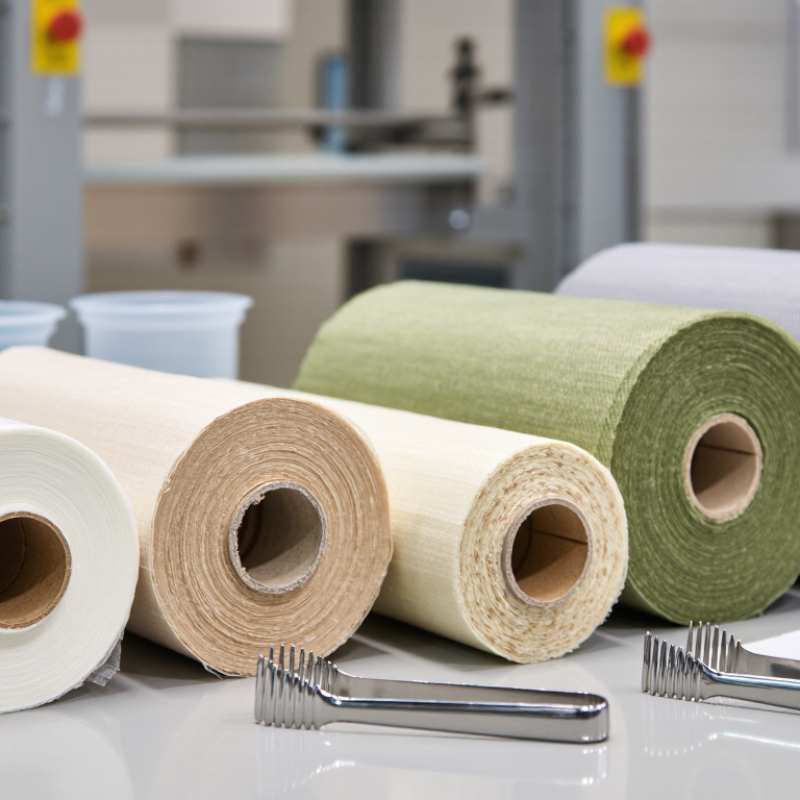
Spunlace nonwoven fabric is a soft sheet made without weaving or knitting. It is also called hydroentangled fabric. Short fibers are arranged into a loose web, then bonded by high-pressure water jets. The water tangles the fibers through the sheet. No traditional yarn is required.
Manufacturing starts with fiber selection and opening. Common choices include polyester, viscose, cotton, and blended fibers. Carding forms an even web, while cross-lapping can improve strength in both directions. Water jets then pass through the web repeatedly. The pressure must be controlled carefully. Too little pressure may leave weak areas. Too much pressure can damage the structure. After hydroentanglement, the fabric is dewatered, dried, and sometimes treated for absorbency, softness, or tear resistance. Quality checks usually measure weight, thickness, tensile strength, absorbency, and lint release. Real production is rarely perfect.
Tips: Match the fiber blend to the end use. Viscose often improves softness and absorbency, while polyester can support strength and dimensional stability. Ask for test data, not only a sample appearance. Check whether the fabric remains stable after wetting, folding, or repeated handling. Buyers should also confirm roll width, basis weight, packaging, and production consistency. A fabric that feels excellent today may perform differently between batches. That detail deserves attention.
2026 Best Spunlace Nonwoven Fabric Types for Buyers? - What Is Spunlace Nonwoven Fabric and How Is It Made?
| Spunlace Fabric Type | Typical Fiber Composition | Typical Basis Weight | Key Characteristics | Common Applications | Buyer Considerations |
|---|---|---|---|---|---|
| Viscose Spunlace | 100% viscose or viscose blended with polyester | 30–120 g/m² | Soft hand feel, high absorbency, good drape, and low lint potential when properly bonded | Wet wipes, facial wipes, cosmetic pads, hygiene products, and medical disposables | Check wet strength, biodegradability claims, pulp source, and compatibility with the intended lotion or cleaning solution |
| Polyester Spunlace | 100% polyester | 30–150 g/m² | High tensile strength, abrasion resistance, dimensional stability, and low moisture absorption | Industrial wipes, filtration support layers, synthetic leather substrates, and durable cleaning cloths | Suitable for repeated handling; verify static control, thermal stability, and liquid absorption requirements |
| Polyester–Viscose Blend | Common blends include 50/50 and 70/30 polyester/viscose | 35–100 g/m² | Balances absorbency, softness, strength, and cost | General-purpose wipes, healthcare textiles, personal-care wipes, and household cleaning products | Specify the exact blend ratio because performance changes significantly with fiber composition |
| Wood-Pulp Composite Spunlace | Wood pulp combined with polyester, viscose, or another reinforcing fiber | 40–120 g/m² | High liquid-holding capacity, good softness, and improved strength compared with loose pulp webs | Dry wipes, industrial absorbent wipes, food-service wipes, and surface-cleaning products | Confirm flushability or dispersibility separately; wood-pulp content alone does not make a product flushable |
| Cotton Spunlace | Cotton or cotton blended with regenerated or synthetic fibers | 40–150 g/m² | Natural feel, good absorbency, and comfortable skin contact | Cosmetic wipes, medical pads, personal-care products, and premium cleaning cloths | Check fiber cleanliness, neps, lint, absorbency, and any required sterilization compatibility |
| Bamboo-Viscose Spunlace | Regenerated cellulose fiber made from bamboo-derived pulp | 30–100 g/m² | Soft, absorbent, and suitable for disposable personal-care products | Facial wipes, baby wipes, cosmetic sheets, and hygiene products | Describe it accurately as regenerated cellulose; verify sourcing and environmental documentation |
| Biodegradable Cellulosic Spunlace | Viscose, lyocell, cotton, wood pulp, or combinations of cellulosic fibers | 35–100 g/m² | Renewable-fiber positioning, softness, and good absorbency; actual end-of-life behavior depends on construction and additives | Compostable-wipe concepts, cosmetic wipes, hygiene products, and sustainable packaging components | Require recognized biodegradation or compostability test evidence rather than relying only on fiber names |
| Hydrophilic Spunlace | Cellulosic, synthetic, or blended fibers with hydrophilic treatment or naturally absorbent fibers | 30–120 g/m² | Rapid wetting and liquid uptake | Wipes, absorbent medical products, liquid-handling materials, and filtration pre-layers | Request strike-through, absorption rate, total absorbency, and wet tensile test results |
| Hydrophobic Spunlace | Mainly polyester or polypropylene-based fibers, sometimes with a water-repellent finish | 30–150 g/m² | Reduced water wetting, good strength, and improved resistance to liquid penetration | Protective covers, industrial wipes, barrier layers, and selected medical components | Confirm hydrostatic pressure, spray rating, breathability, and chemical compatibility |
| Perforated or Patterned Spunlace | Viscose, polyester, wood pulp composites, or blended fibers | 35–120 g/m² | Engineered apertures or surface patterns improve texture, lotion distribution, wiping efficiency, or tear control | Facial masks, cosmetic sheets, textured wipes, and specialty cleaning cloths | Evaluate pattern uniformity, edge integrity, elongation, and converting performance |
How Spunlace Nonwoven Fabric Is Made
| Production Stage | Process Description | Important Buyer Quality Checks |
|---|---|---|
| 1. Fiber Preparation | Fibers are opened, blended, and cleaned to achieve the required composition and uniformity. | Fiber type, blend ratio, fiber length, cleanliness, and contamination control |
| 2. Web Formation | Carding, air-laid, or wet-laid equipment forms a loose web with the target basis weight and fiber orientation. | Basis-weight consistency, web uniformity, thickness, and machine-direction strength |
| 3. Hydroentanglement | Fine, high-pressure water jets entangle the fibers mechanically. No chemical binder is normally required for standard spunlace bonding. | Bonding uniformity, fiber release, tensile strength, elongation, and surface appearance |
| 4. Dewatering and Drying | Water is removed through suction and drying systems, while the fabric is stabilized for winding. | Residual moisture, shrinkage, curling, odor, and roll hardness |
| 5. Finishing and Converting | The material may receive treatments such as hydrophilic or hydrophobic finishing, perforation, embossing, slitting, or cutting. | Finish add-on, absorbency, odor, width tolerance, roll length, and packaging integrity |
Core Specifications Buyers Should Compare
| Specification | Why It Matters | Recommended Purchasing Practice |
|---|---|---|
| Basis Weight | Affects coverage, thickness, absorbency, strength, and material cost. | Define the target value and permitted tolerance in the specification. |
| Thickness and Density | Influences softness, cushioning, liquid holding, and converting behavior. | Test at a stated pressure because thickness changes with test conditions. |
| Tensile Strength and Elongation | Determines resistance to tearing and stretching during use and converting. | Request both machine-direction and cross-direction results, dry and wet where relevant. |
| Absorbency and Wetting Rate | Critical for wipes, medical materials, and liquid-handling products. | Use a defined test method and test liquid rather than relying on descriptive terms alone. |
| Lint and Fiber Release | Impacts cleanliness, surface residue, and suitability for sensitive applications. | Set a lint limit and inspect samples after wiping under realistic conditions. |
| Chemical and Skin Compatibility | Finishes, lotions, preservatives, and cleaning chemicals can change fabric performance. | Test the finished product system, not only the untreated fabric. |
| Sustainability Claims | Fiber origin, additives, packaging, and disposal route all affect environmental performance. | Request supporting test reports and clearly distinguish biodegradable, compostable, recyclable, and flushable claims. |